
Profile 01

Integrated chemicals and recovery capability
The company combines high-purity electronic chemicals, specialty chemicals, fine chemicals, and solvent recovery within one coordinated operating platform.
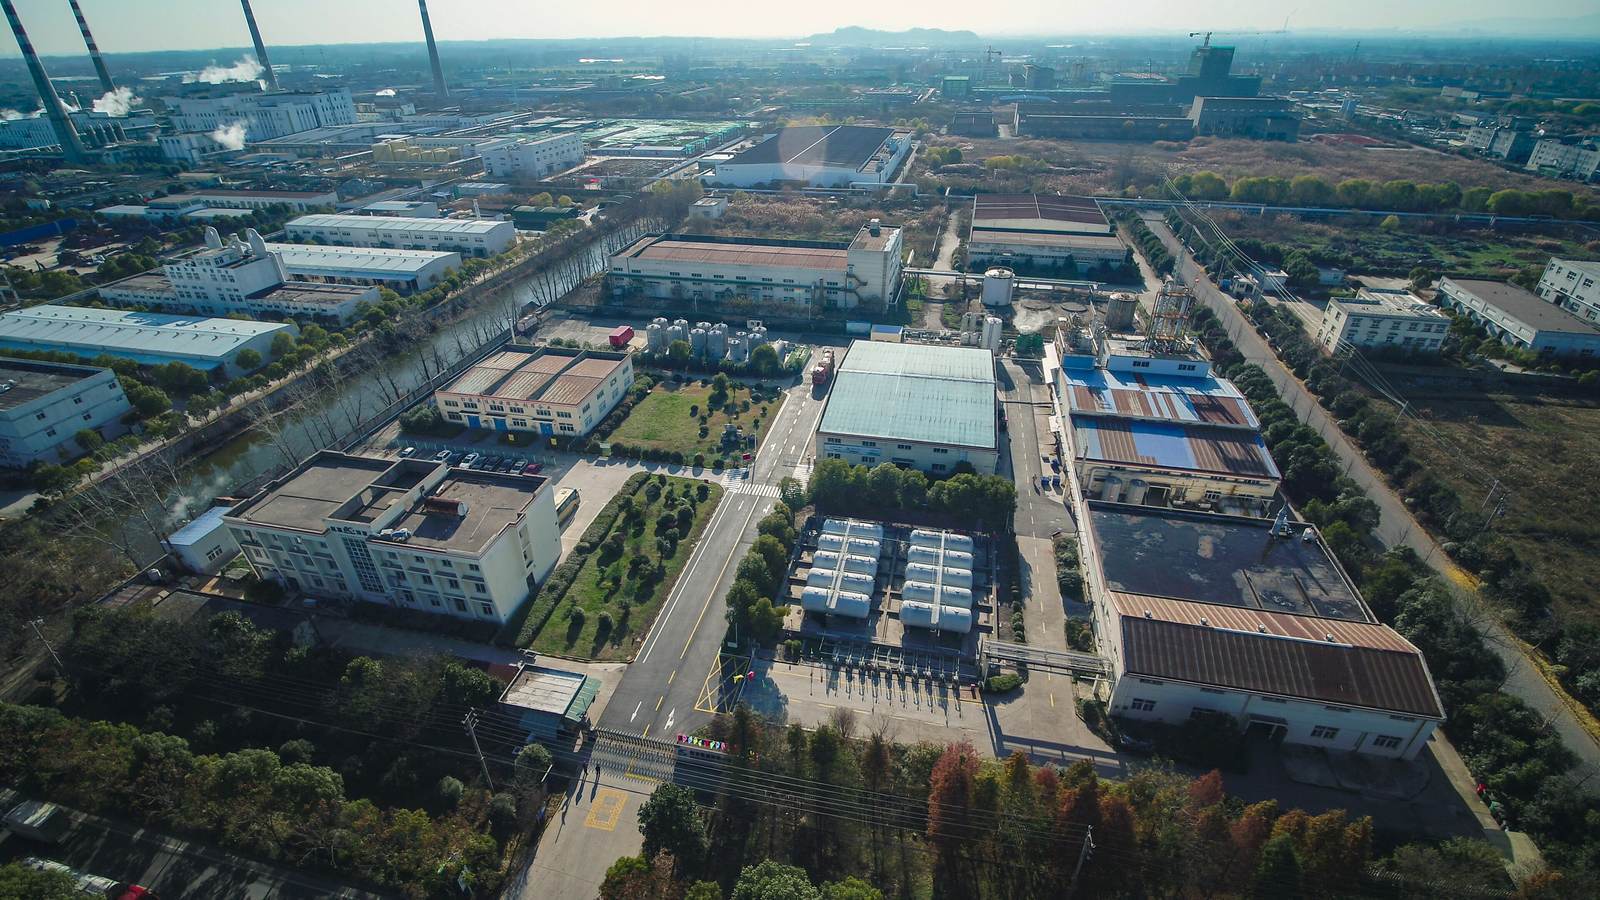
About Kaiyan
Nanjing Kaiyan Environmental Technology Co., Ltd. is a high-tech chemical enterprise integrating R&D, manufacturing, trading, and hazardous-waste resource recovery, with strengths in high-purity electronic chemicals, specialty chemicals, fine chemicals, and spent organic-solvent recycling.
Company Profile
Nanjing Kaiyan Environmental Technology Co., Ltd. provides safe, compliant, and sustainable chemical solutions for industrial customers.
Based in Nanjing, Kaiyan serves domestic and international customers with hazardous chemicals and related industrial services, balancing safety, efficiency, and environmental responsibility. With more than 23 years of experience, the company supports customers across pharmaceuticals, energy, electronics, and advanced manufacturing.
Backed by disciplined quality control, compliant storage and packaging, and dependable logistics execution, Kaiyan delivers end-to-end support spanning chemical supply, custom blending, regulatory coordination, and spent-solvent recovery.
The company continues to strengthen greener operating practices across sourcing, warehousing, processing, and distribution while maintaining rigorous standards for safety, quality, and traceability.
Kaiyan aims to become a leading enterprise in integrated resource utilization by continuously improving product quality, delivery efficiency, and service responsiveness.
The company combines high-purity electronic chemicals, specialty chemicals, fine chemicals, and solvent recovery within one coordinated operating platform.
Industrial-grade and reagent-grade lines, distillation systems, and solvent-recovery equipment support consistent output and dependable delivery.
Safety, environmental responsibility, warehousing, packaging, and logistics are managed through disciplined compliance workflows.
Milestones
The company was founded in May 2002, marking the beginning of its chemical-products business.
The company passed ISO 9001:2000 quality-management certification in August 2002.
The company acquired 30 mu of land in the Liuhe Hongshan Fine Chemical Park in Nanjing as reserve land for future chemical-industry development.
Construction of the new plant in the Liuhe Hongshan Fine Chemical Park began, with the project planned in two phases.
The new plant obtained the hazardous-waste operating permit for the recycling of spent organic solvents (HW42), initially covering three product varieties.
The company launched an expansion project to add more recycled spent-organic-solvent product varieties under the HW42 category.
The company passed ISO 14001:2004 environmental-management certification.
Phase II construction was launched, including a new Class A warehouse and an integrated office building.
The integrated office building completed under Phase II was finished and officially put into use.
The company completed an upgrade of its recycled-solvent operation.
The company obtained its high-tech enterprise certificate.
The company completed its corporate renaming and brand upgrade.
The company obtained the Level-II enterprise safety-standardization certificate.
The company completed the formal acceptance of the upgrade project.
Storage items were officially added to the company’s operating-license scope.
The transfer of the KaiYan trademark was completed, and the new KaiYan trademark registration was finalized.
Certificates
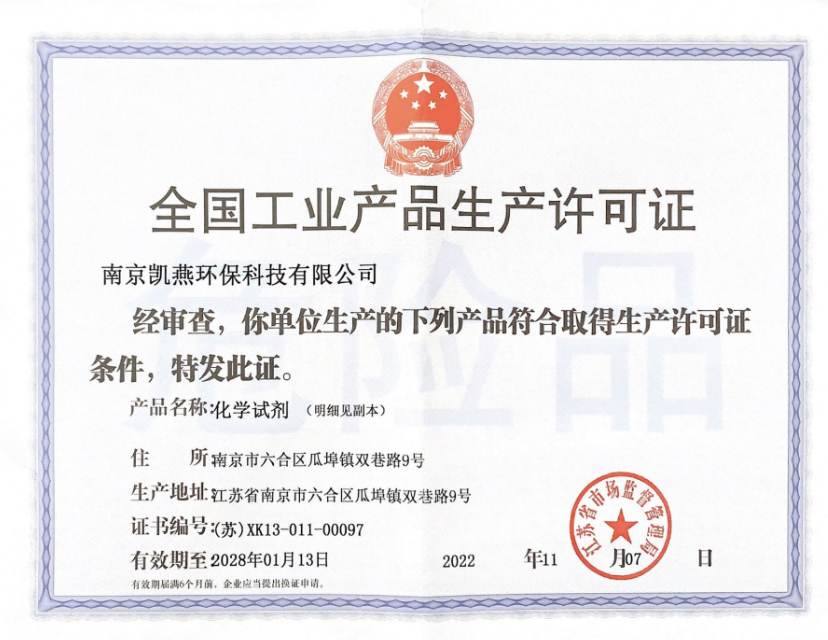
Shows regulated production and industrial operating capability.
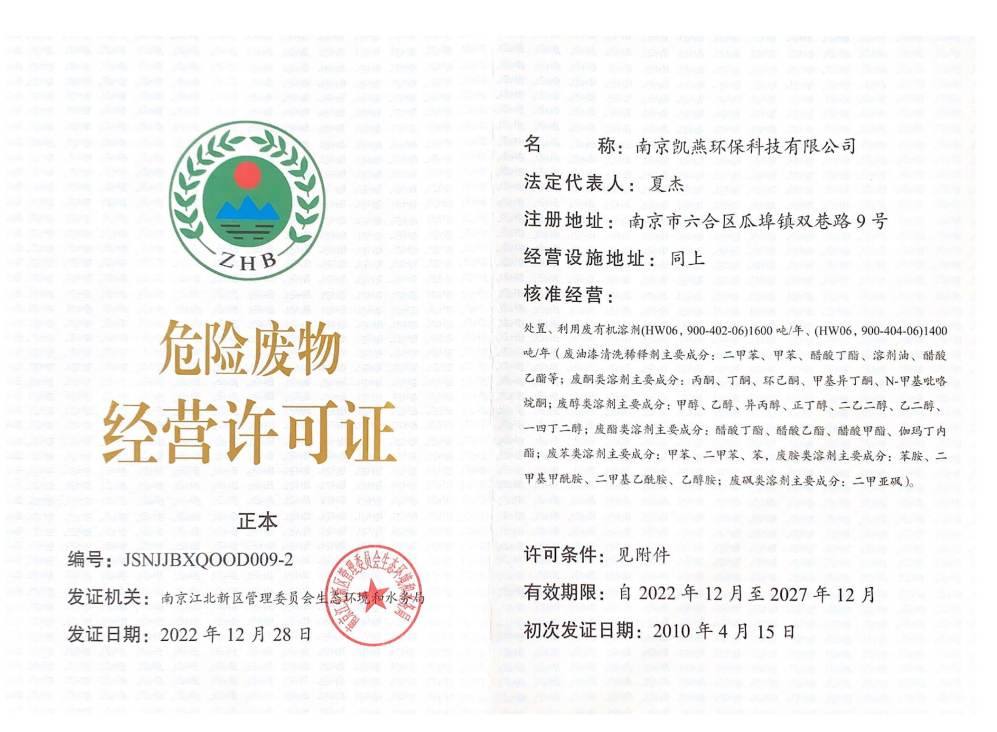
Highlights hazardous-waste operation and disposal qualification.
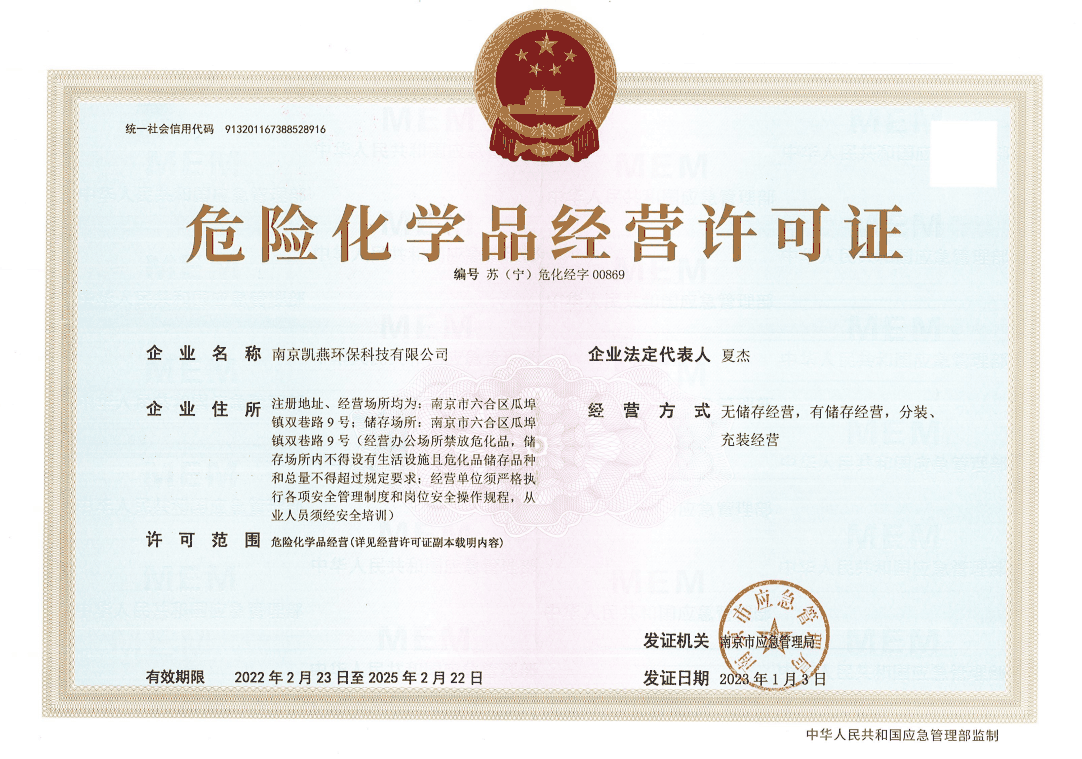
Strengthens compliance confidence for B2B buyers.
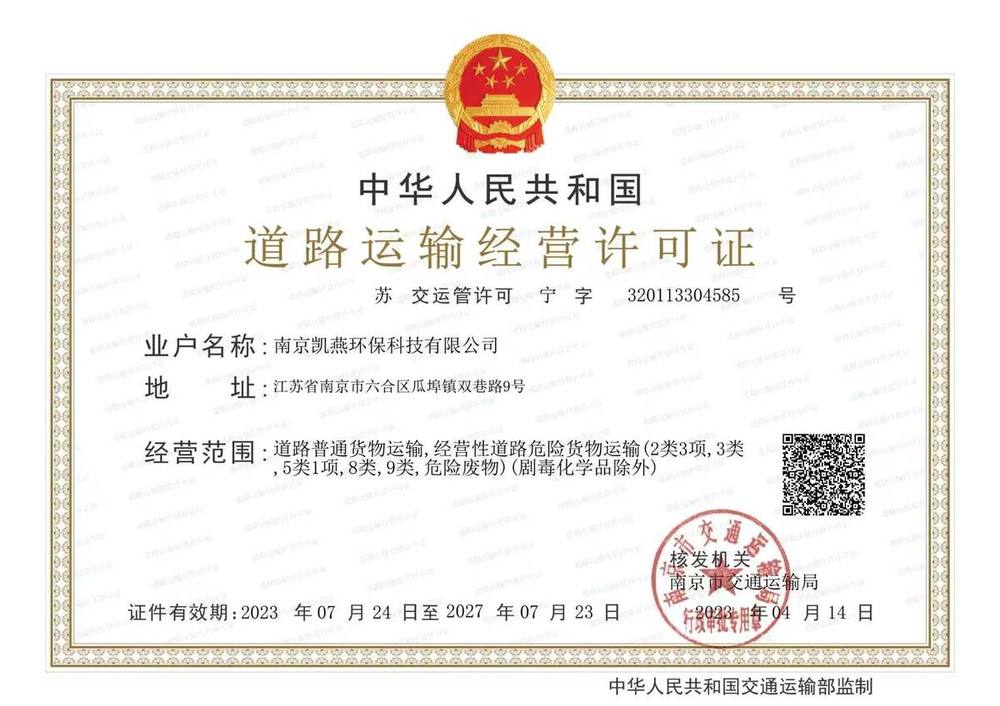
Acts as the legal certificate for compliant road transportation operations.
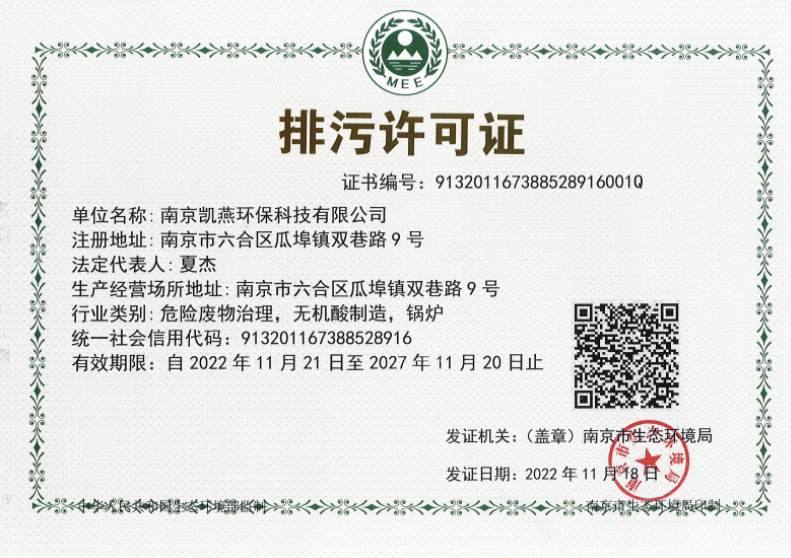
Shows pollutant-discharge authorization and environmental management discipline.
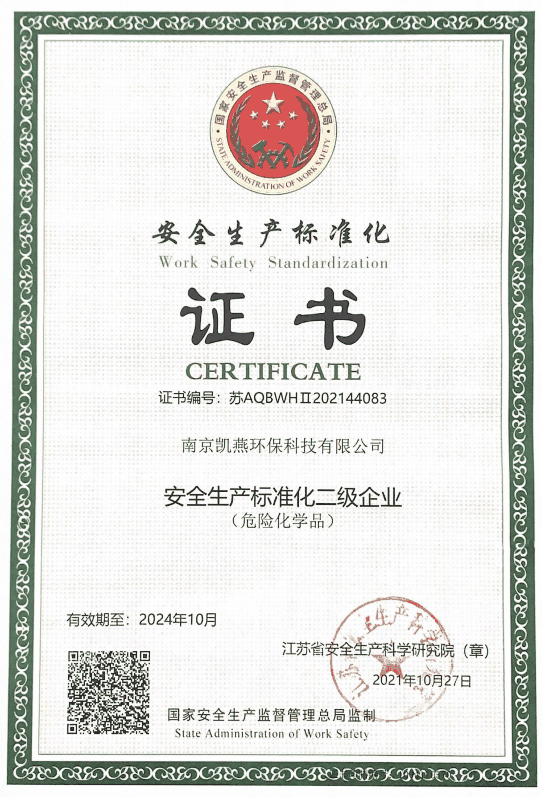
Strengthens the safety management and compliance image.
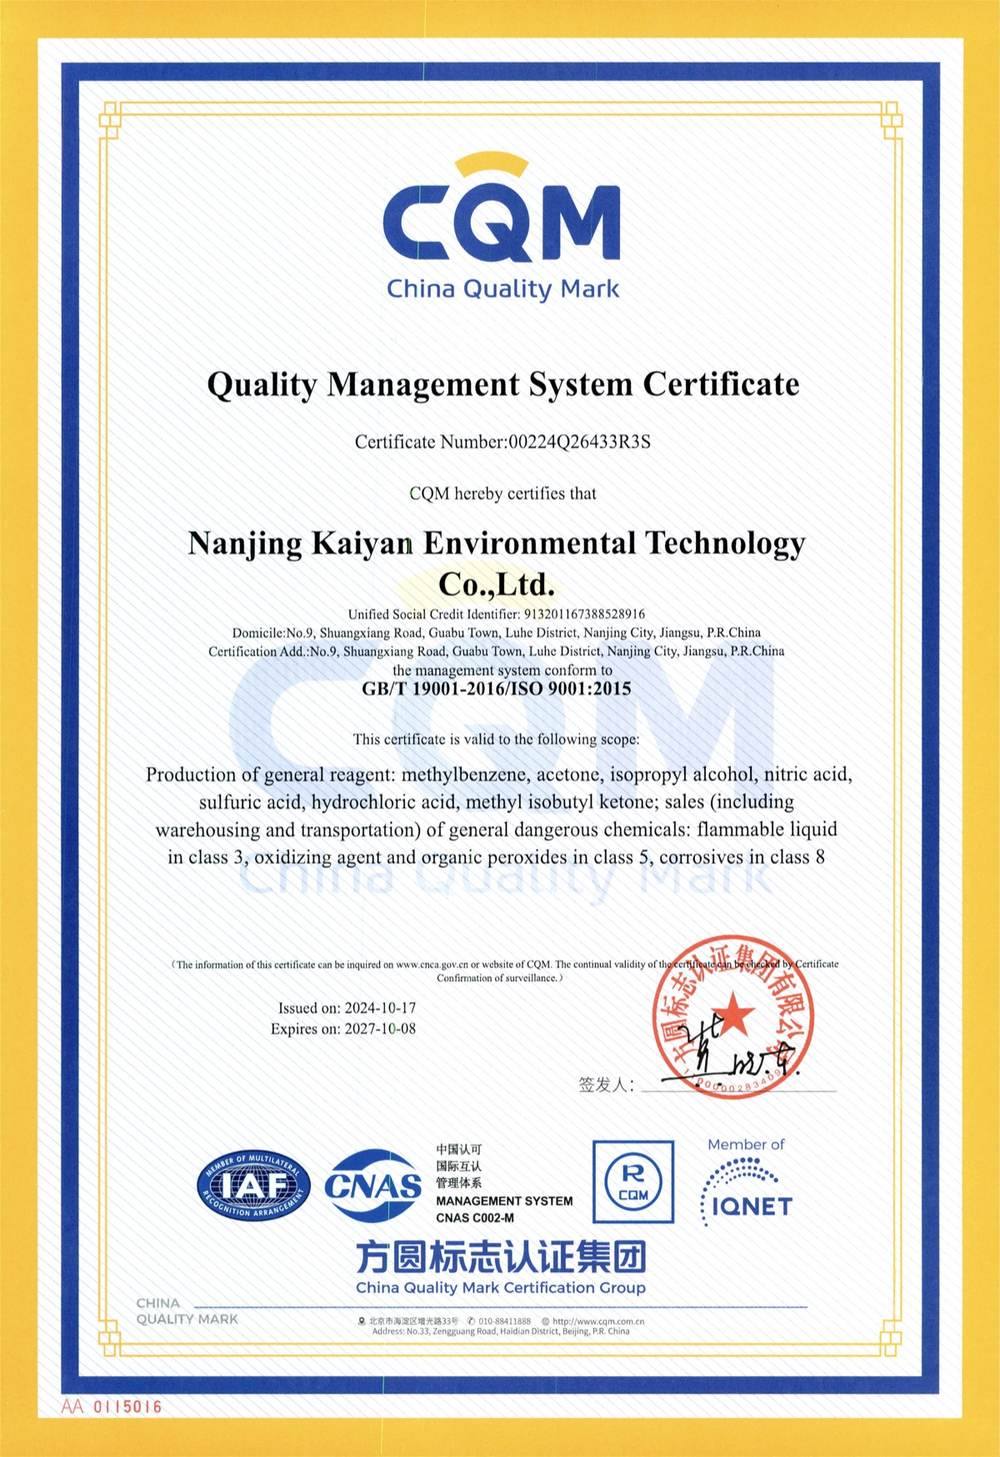
Useful for sustainability and environmental control positioning.
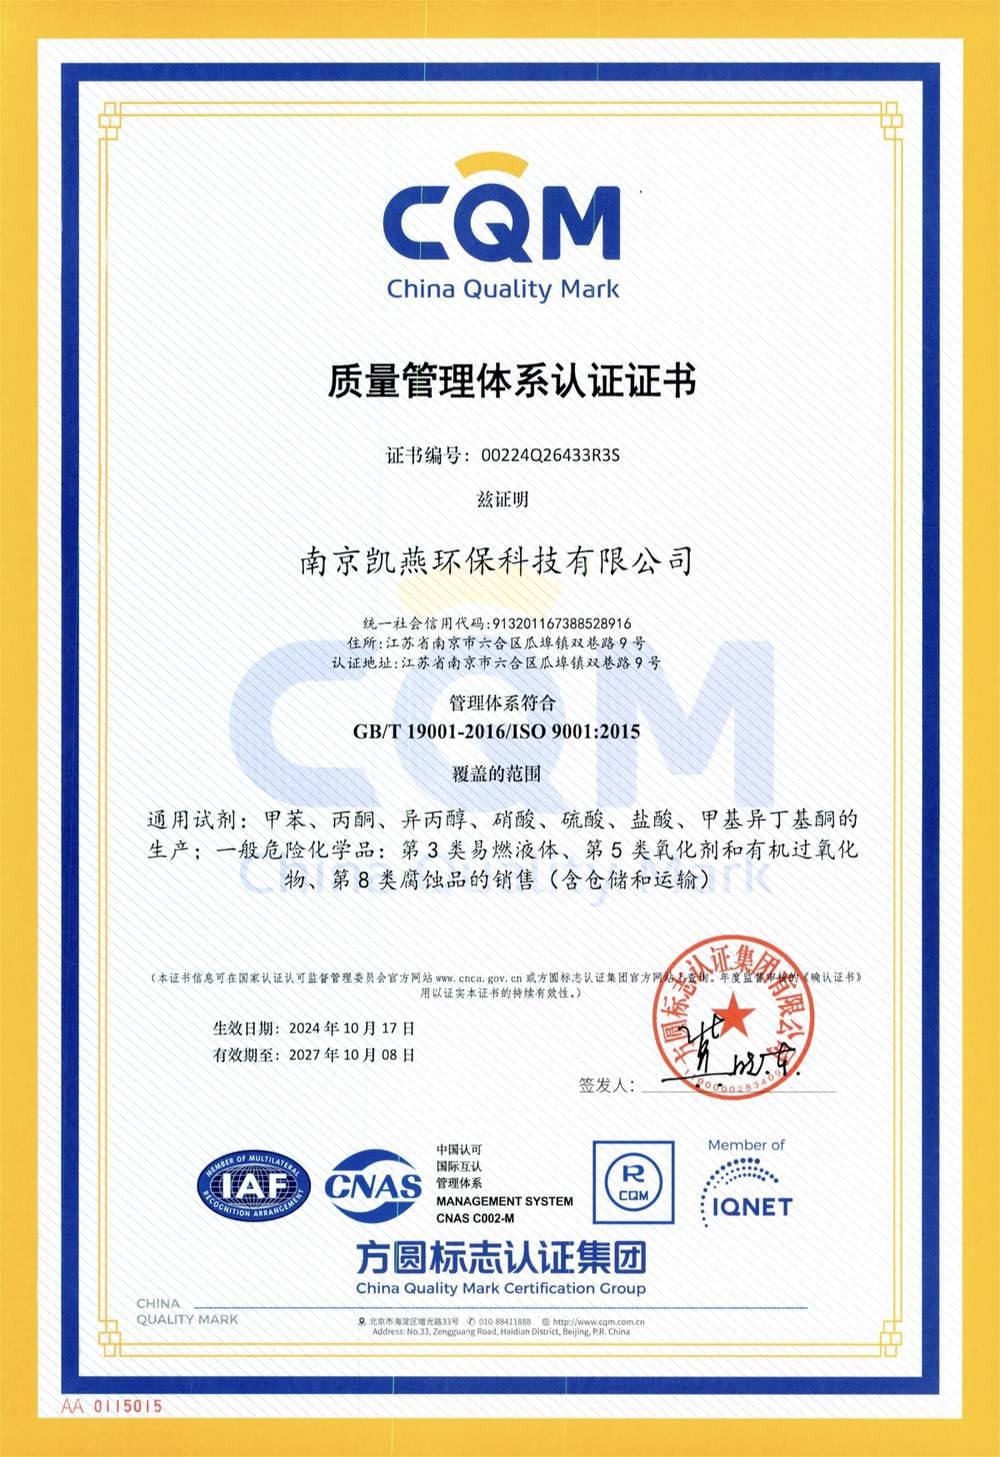
Supports product stability and quality assurance messaging.
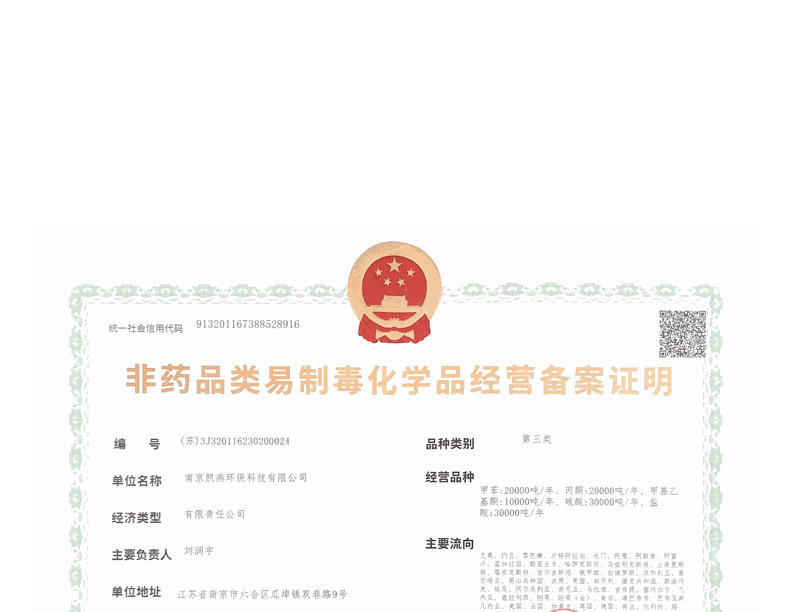
Shows filing and compliant operation capability for category III precursor chemicals.
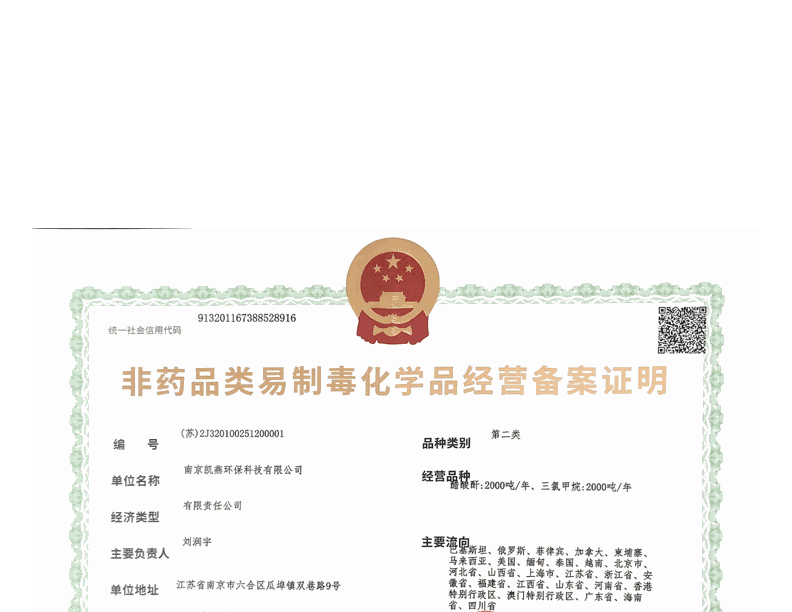
Shows filing qualification for category II non-pharmaceutical precursor chemical operations.
Factory Album
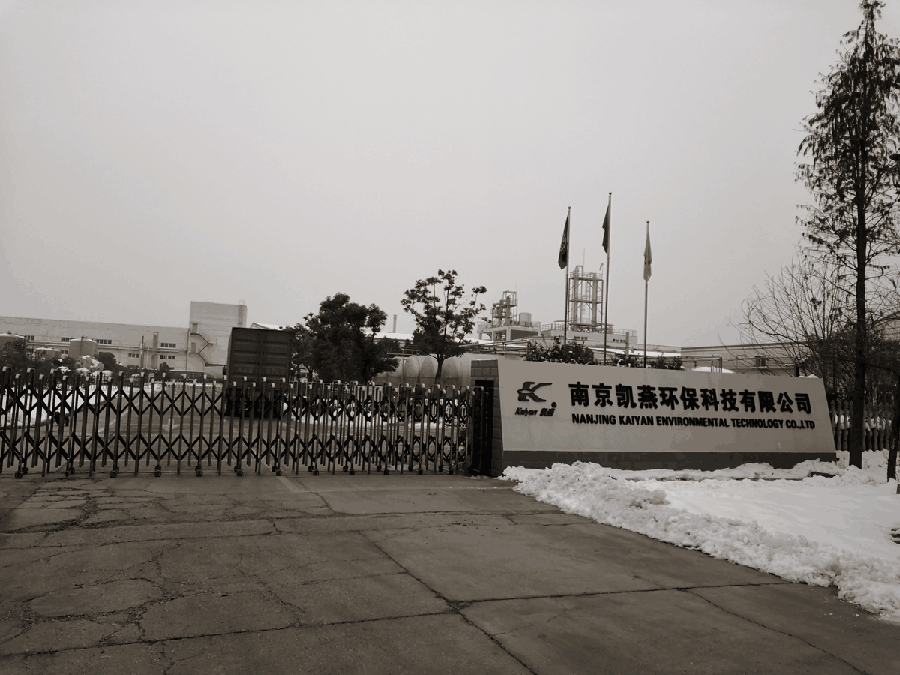
Main gate and brand-facing entrance of the campus.
Overall campus layout with storage and production areas.
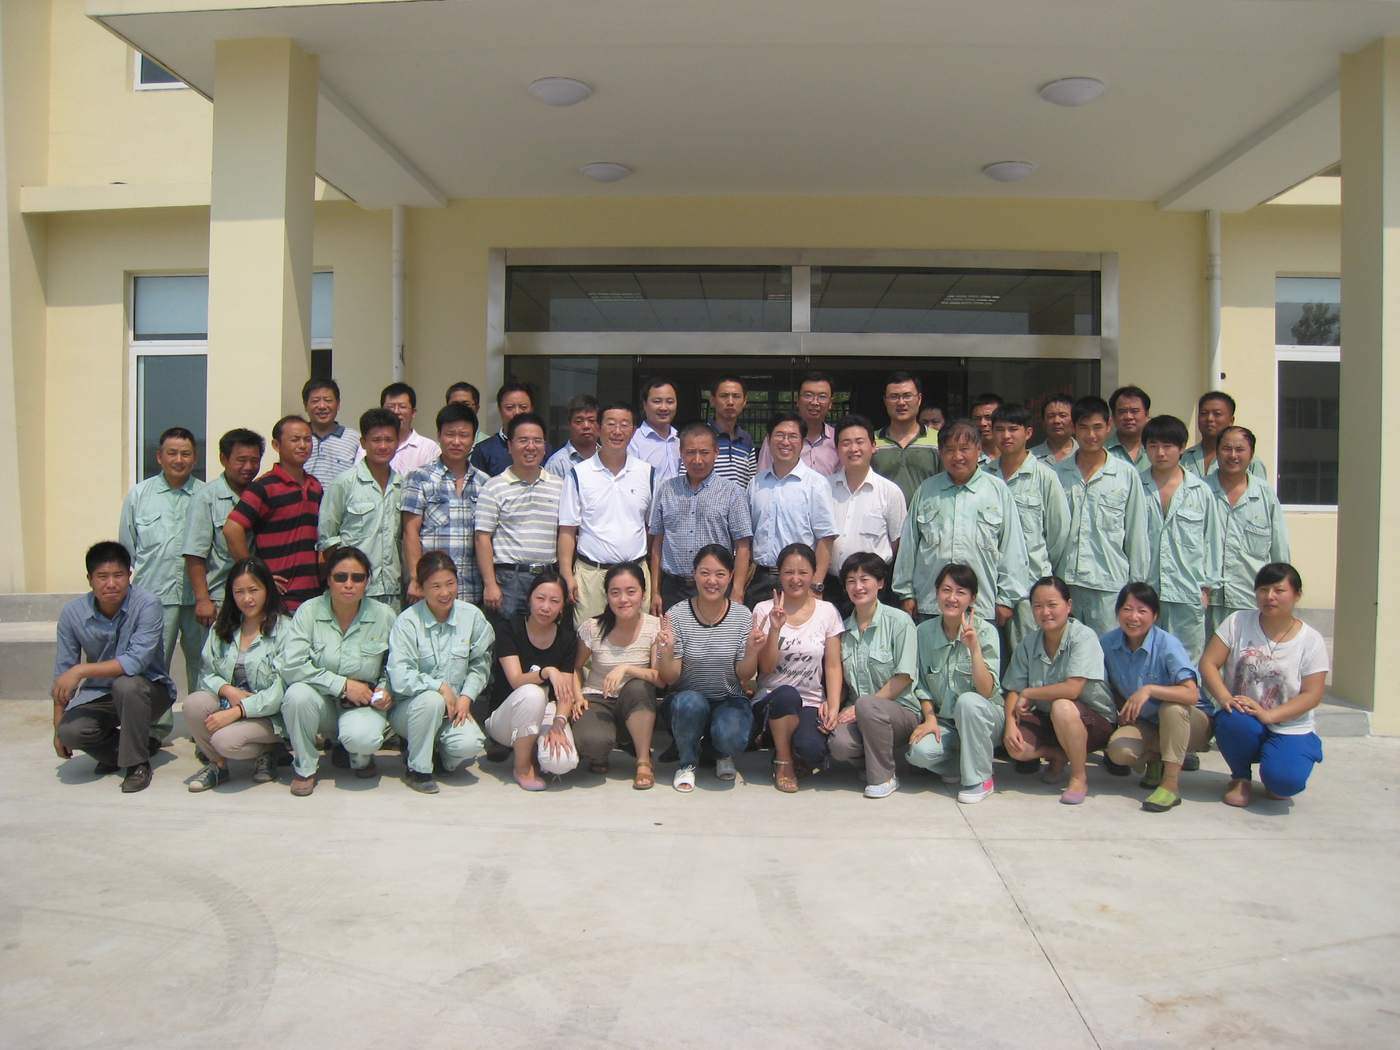
A team photo taken in front of the office building.
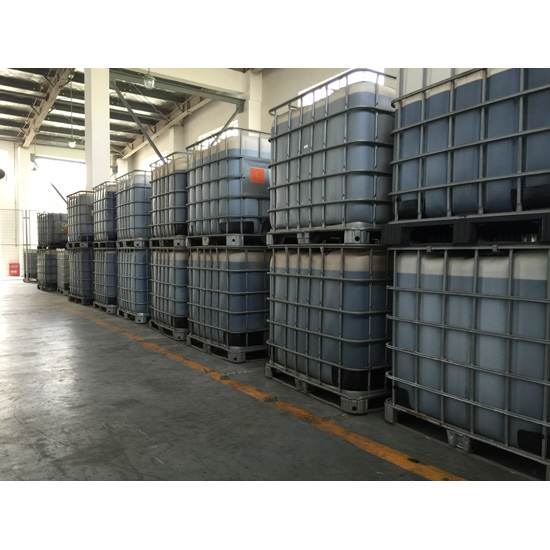
On-site warehousing area.
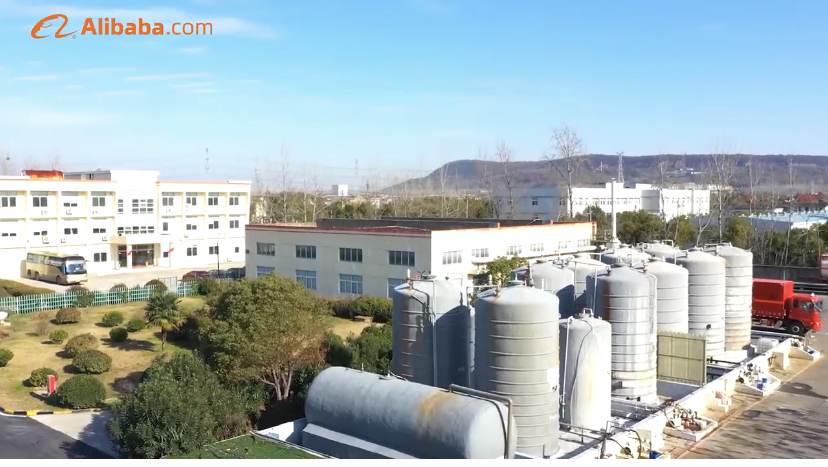
Bulk chemical storage area.
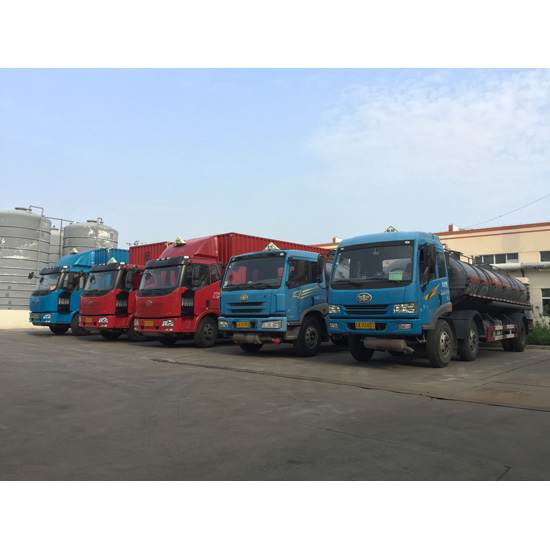
Compliant delivery vehicles and transport capability.
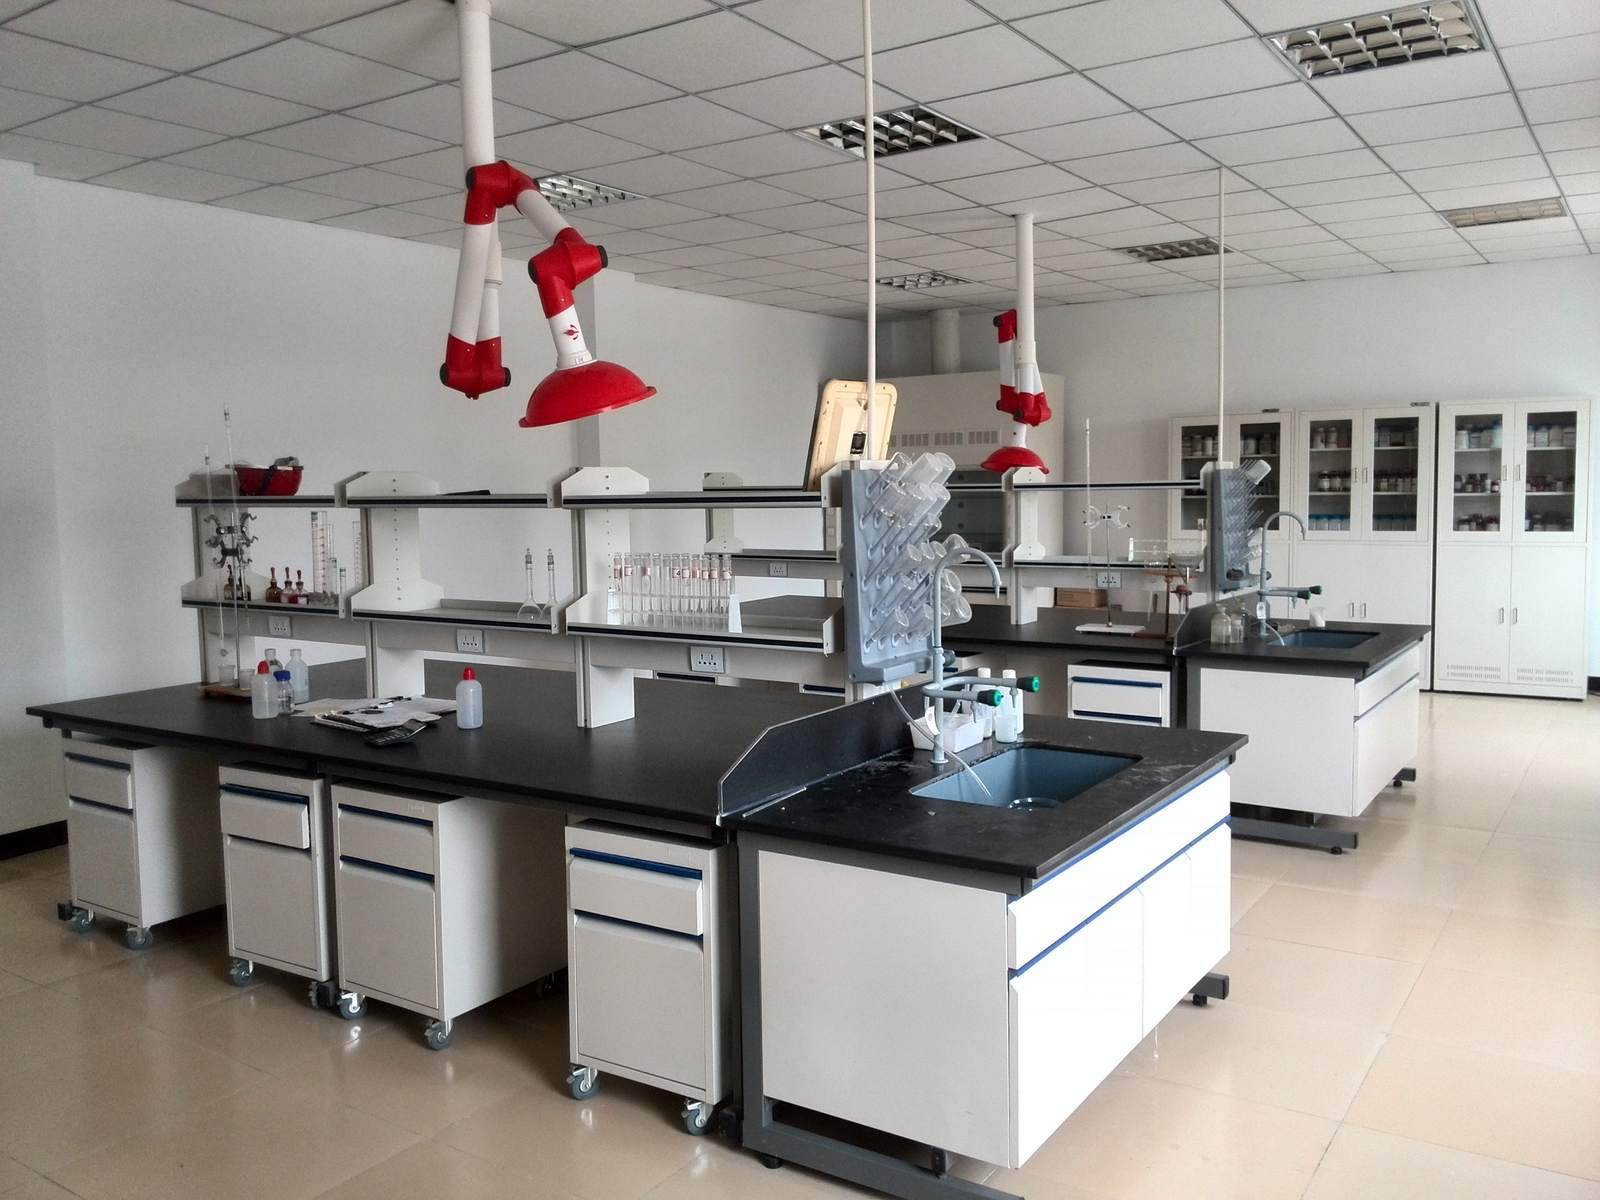
Testing analysis and quality-control environment.
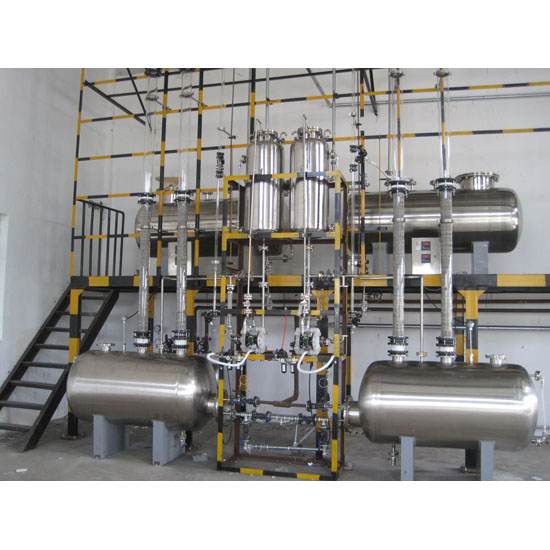
On-site solvent recovery equipment.
Corporate Values
The company emphasizes understanding customer requirements accurately, responding promptly, and delivering dependable service.
The mission connects resource recovery, fine chemicals, and high-purity chemical capabilities to long-term customer value.
The long-term vision is to build a stronger enterprise in resource recovery and integrated chemical services.
The team is committed to continuous improvement, with product quality and service reliability as enduring standards.
Culture Space
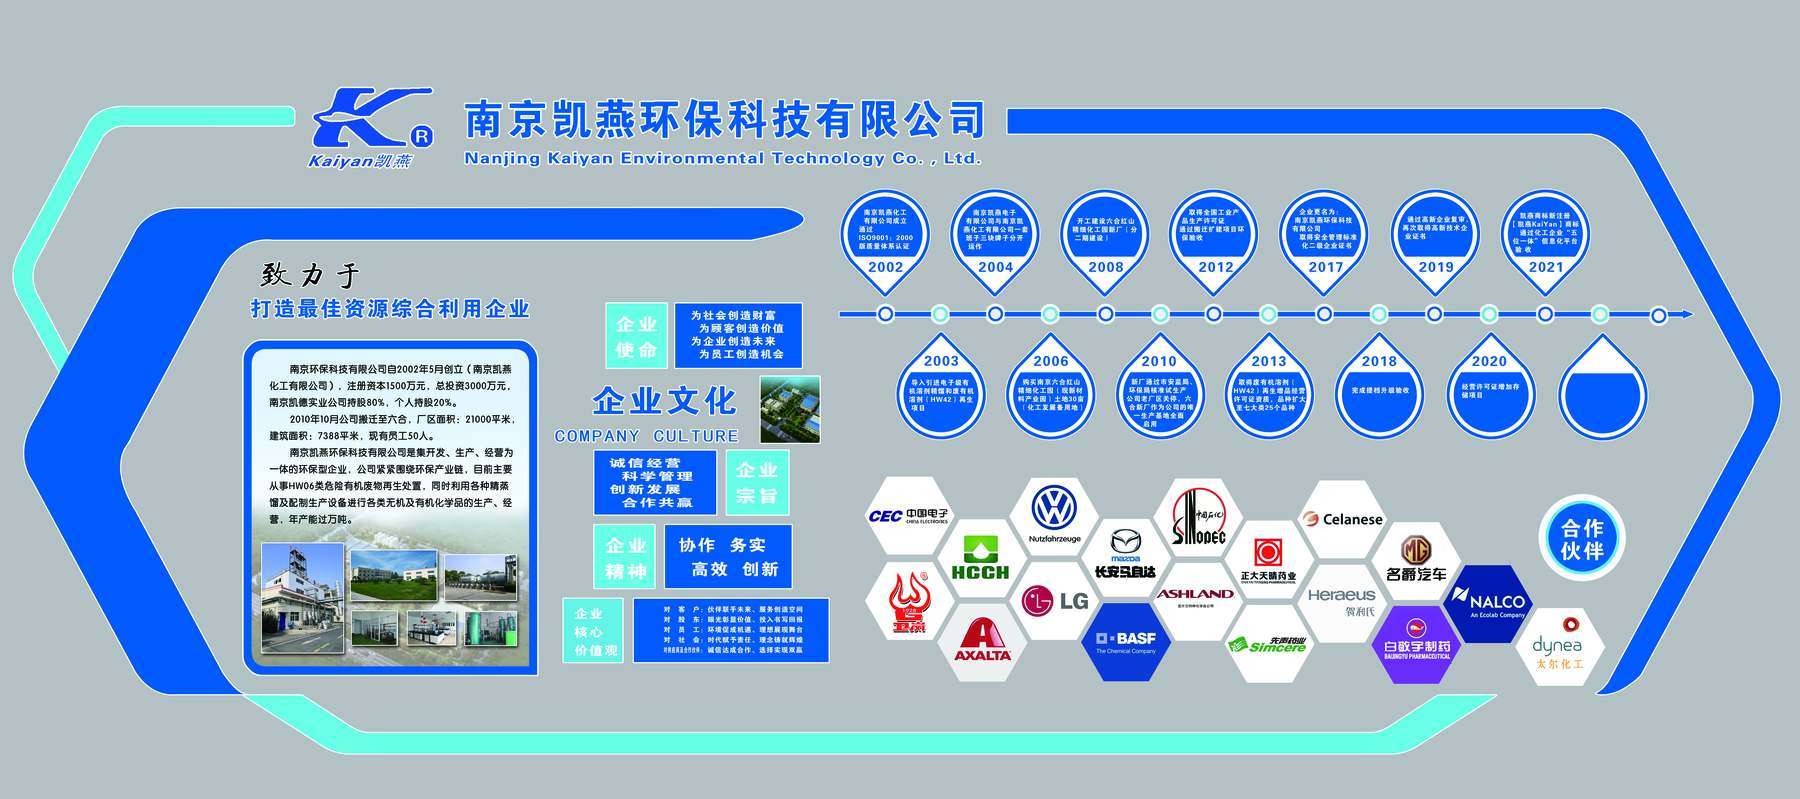
A combined display of company history, values, and partner recognition in the main office entrance area.
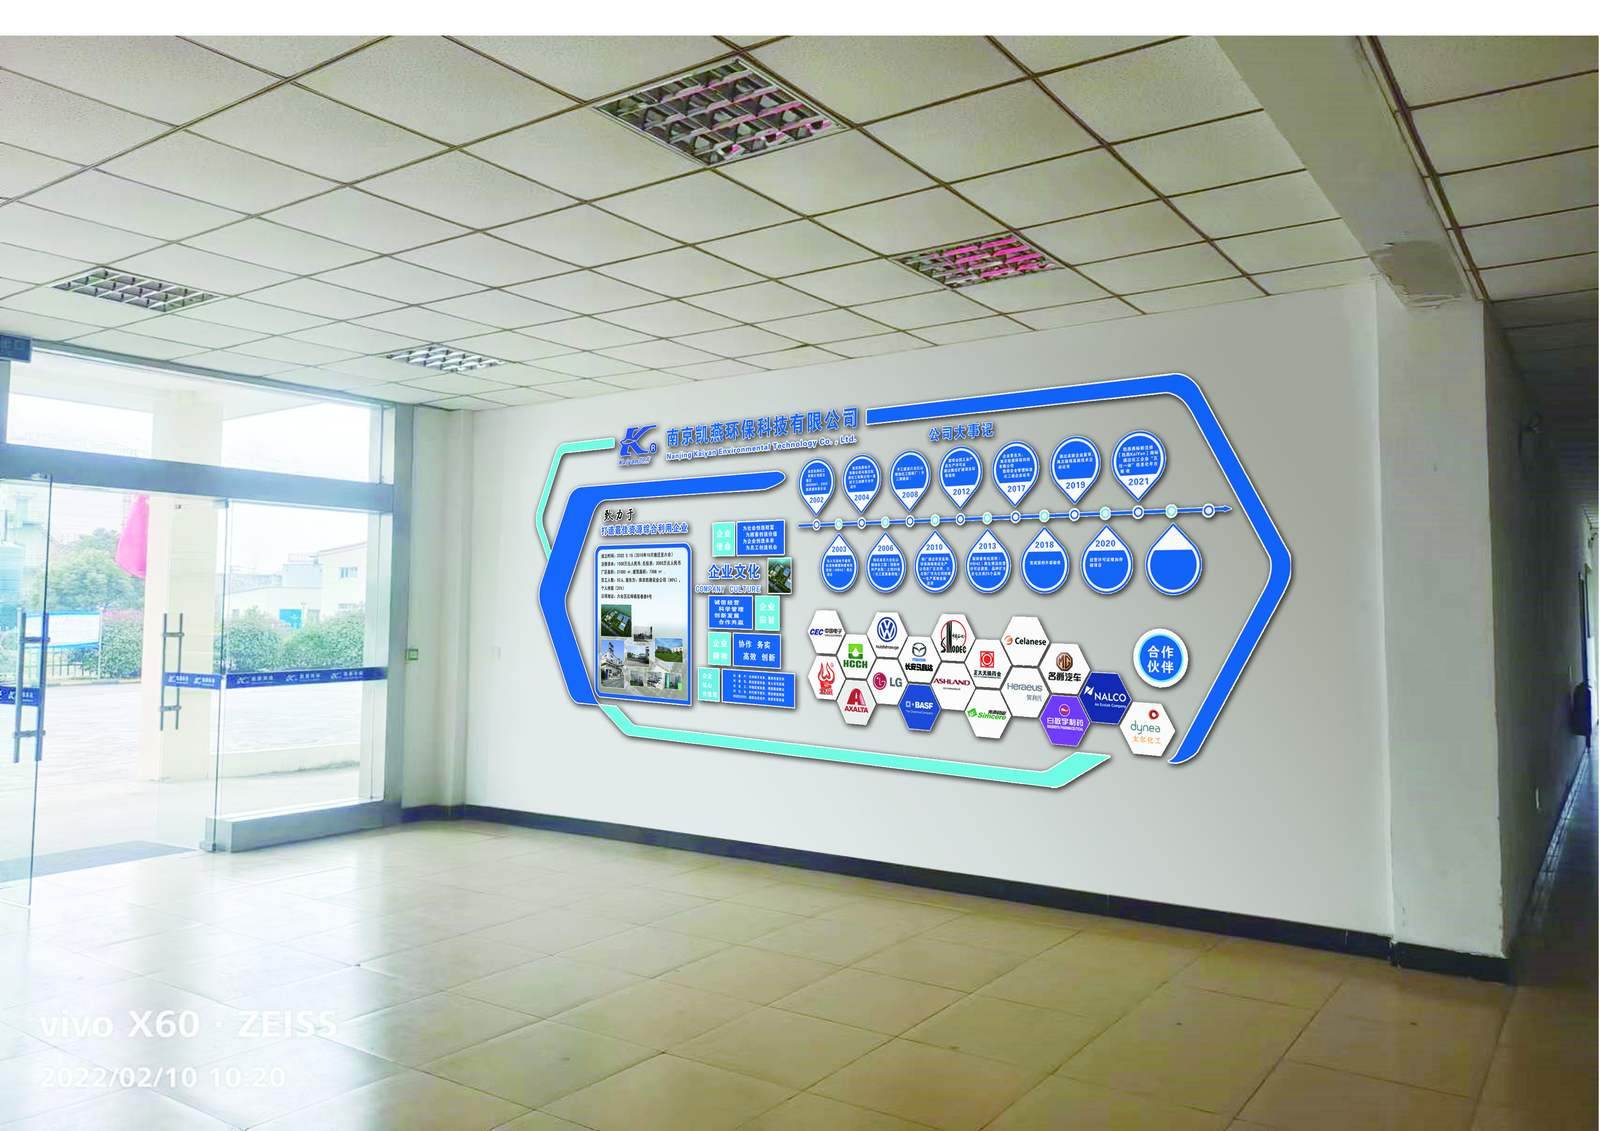
Lobby environment that strengthens visitor reception and internal brand presentation.
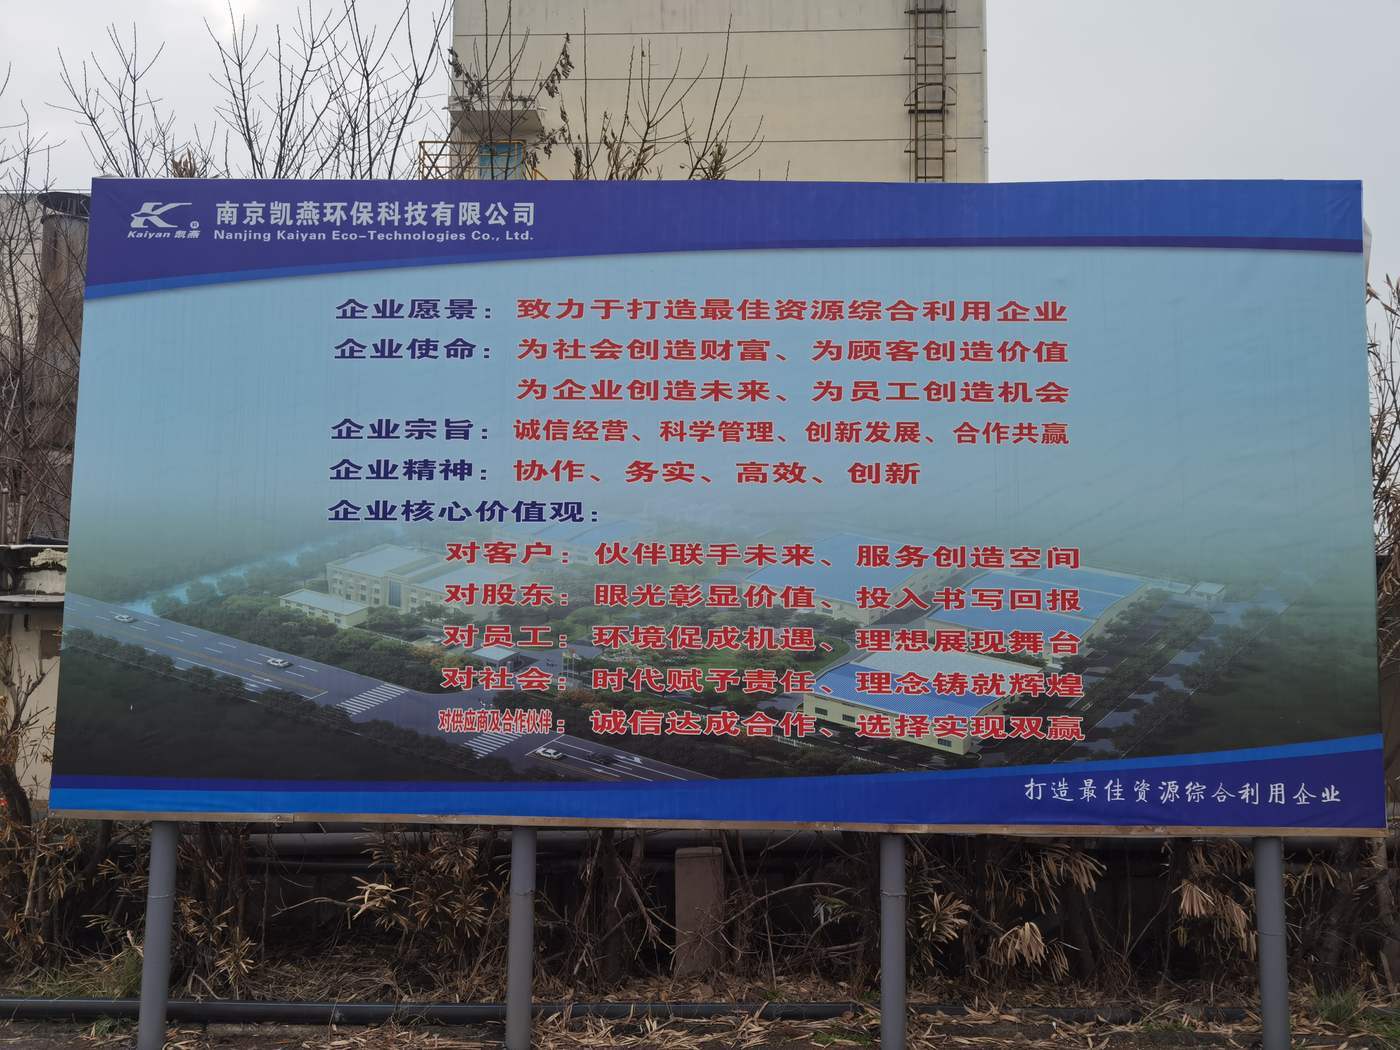
Branded culture poster material that can be used to reinforce identity and values.
Exchange & Activity
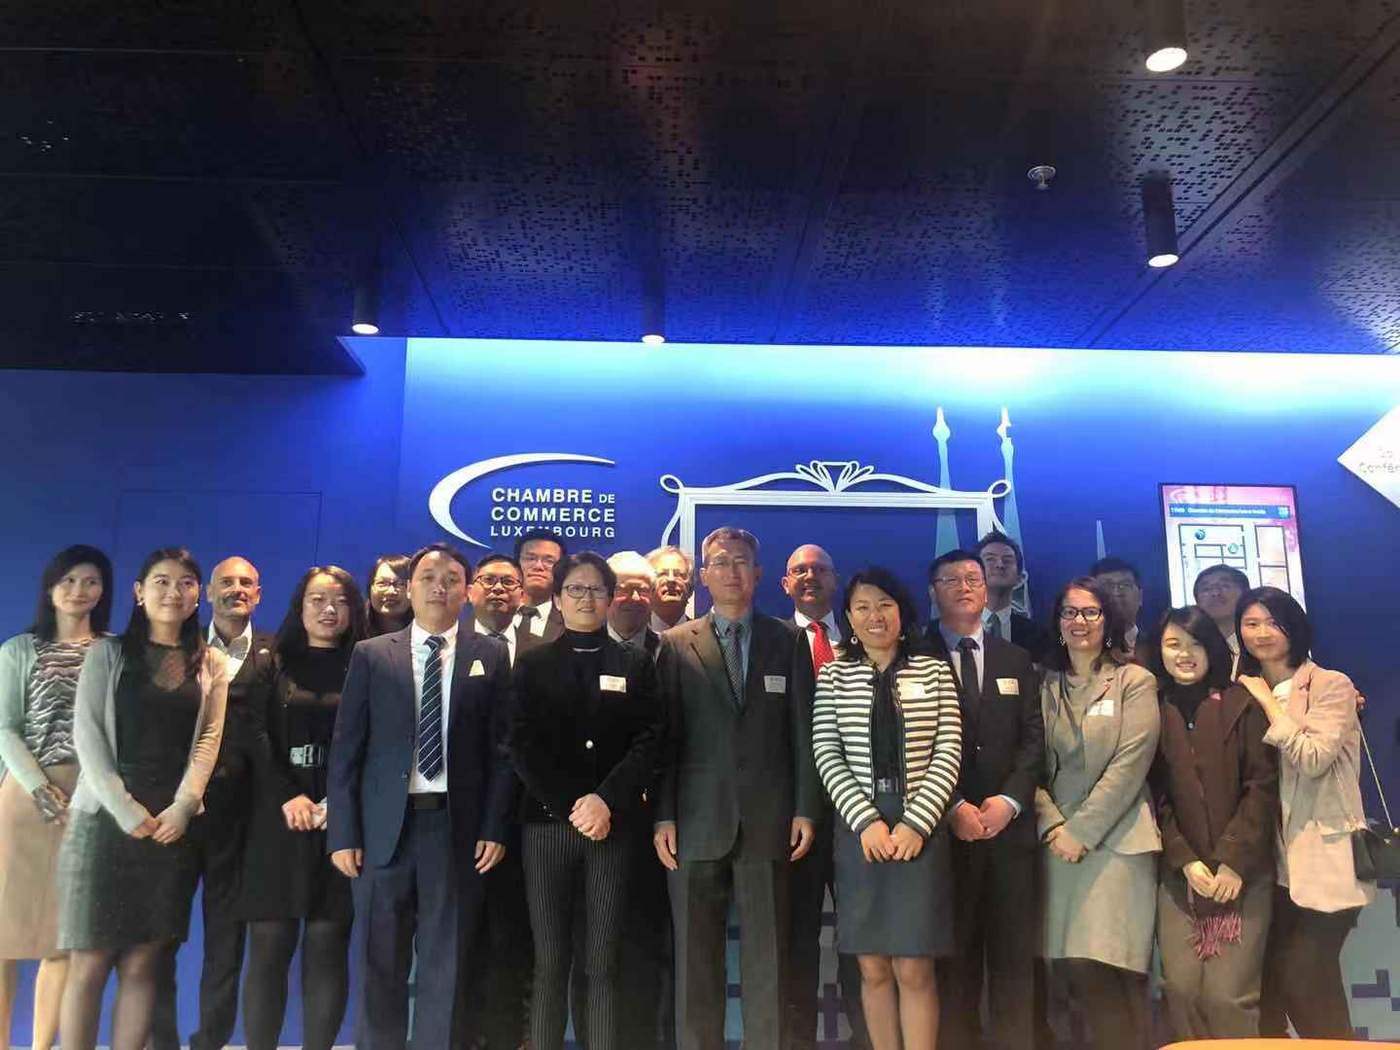
Shows customer-facing communication and market-development activity.
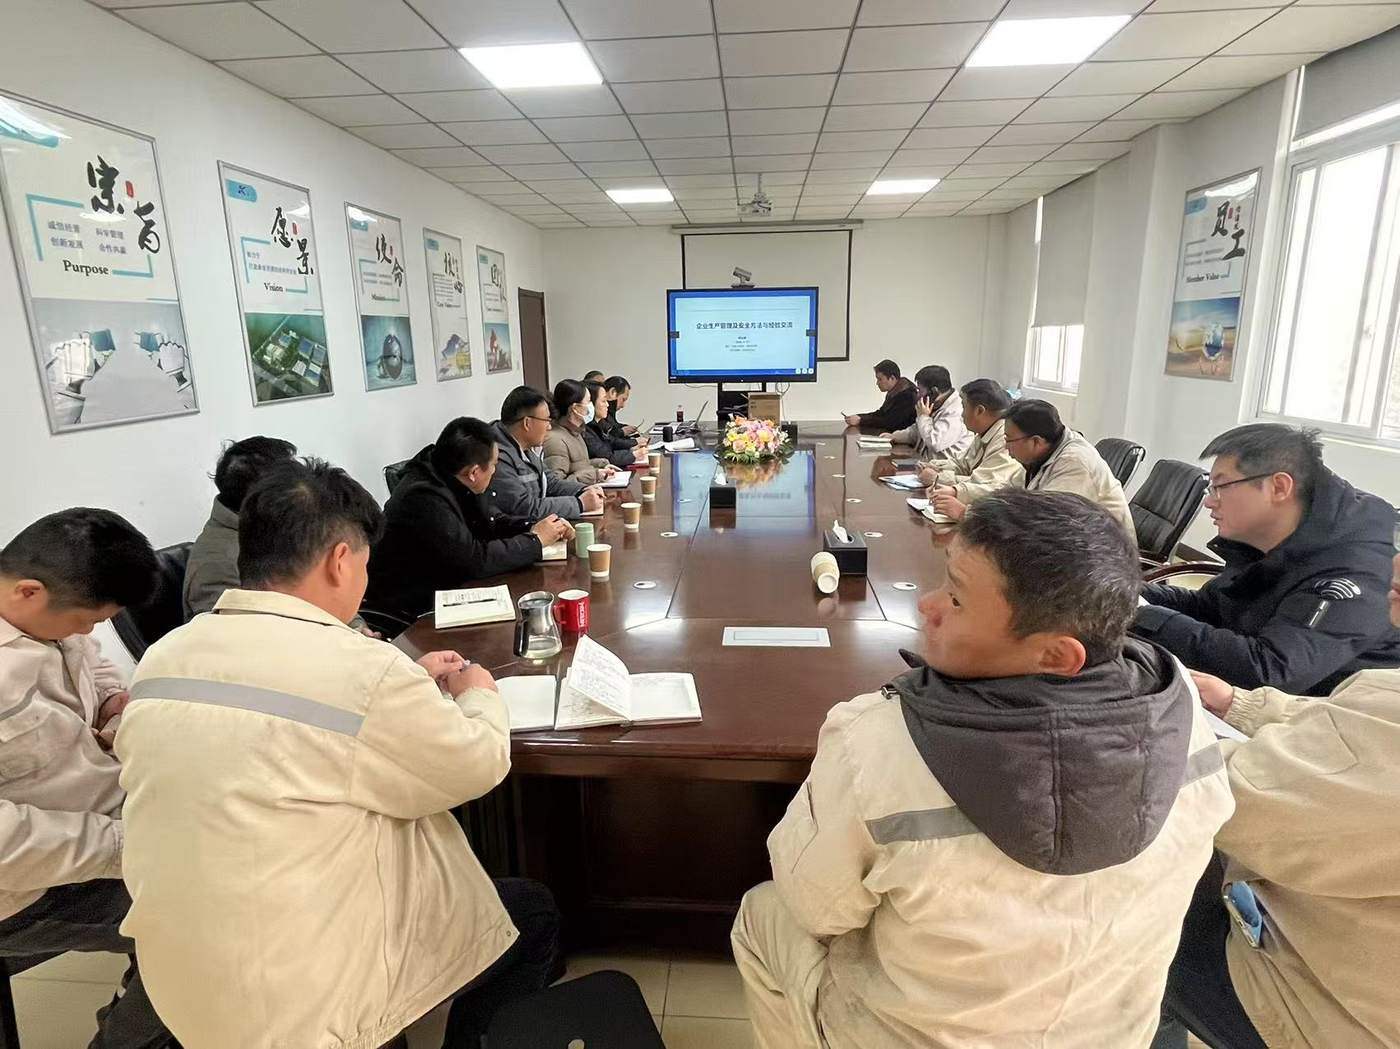
Shows internal training, production management, and safety coordination.
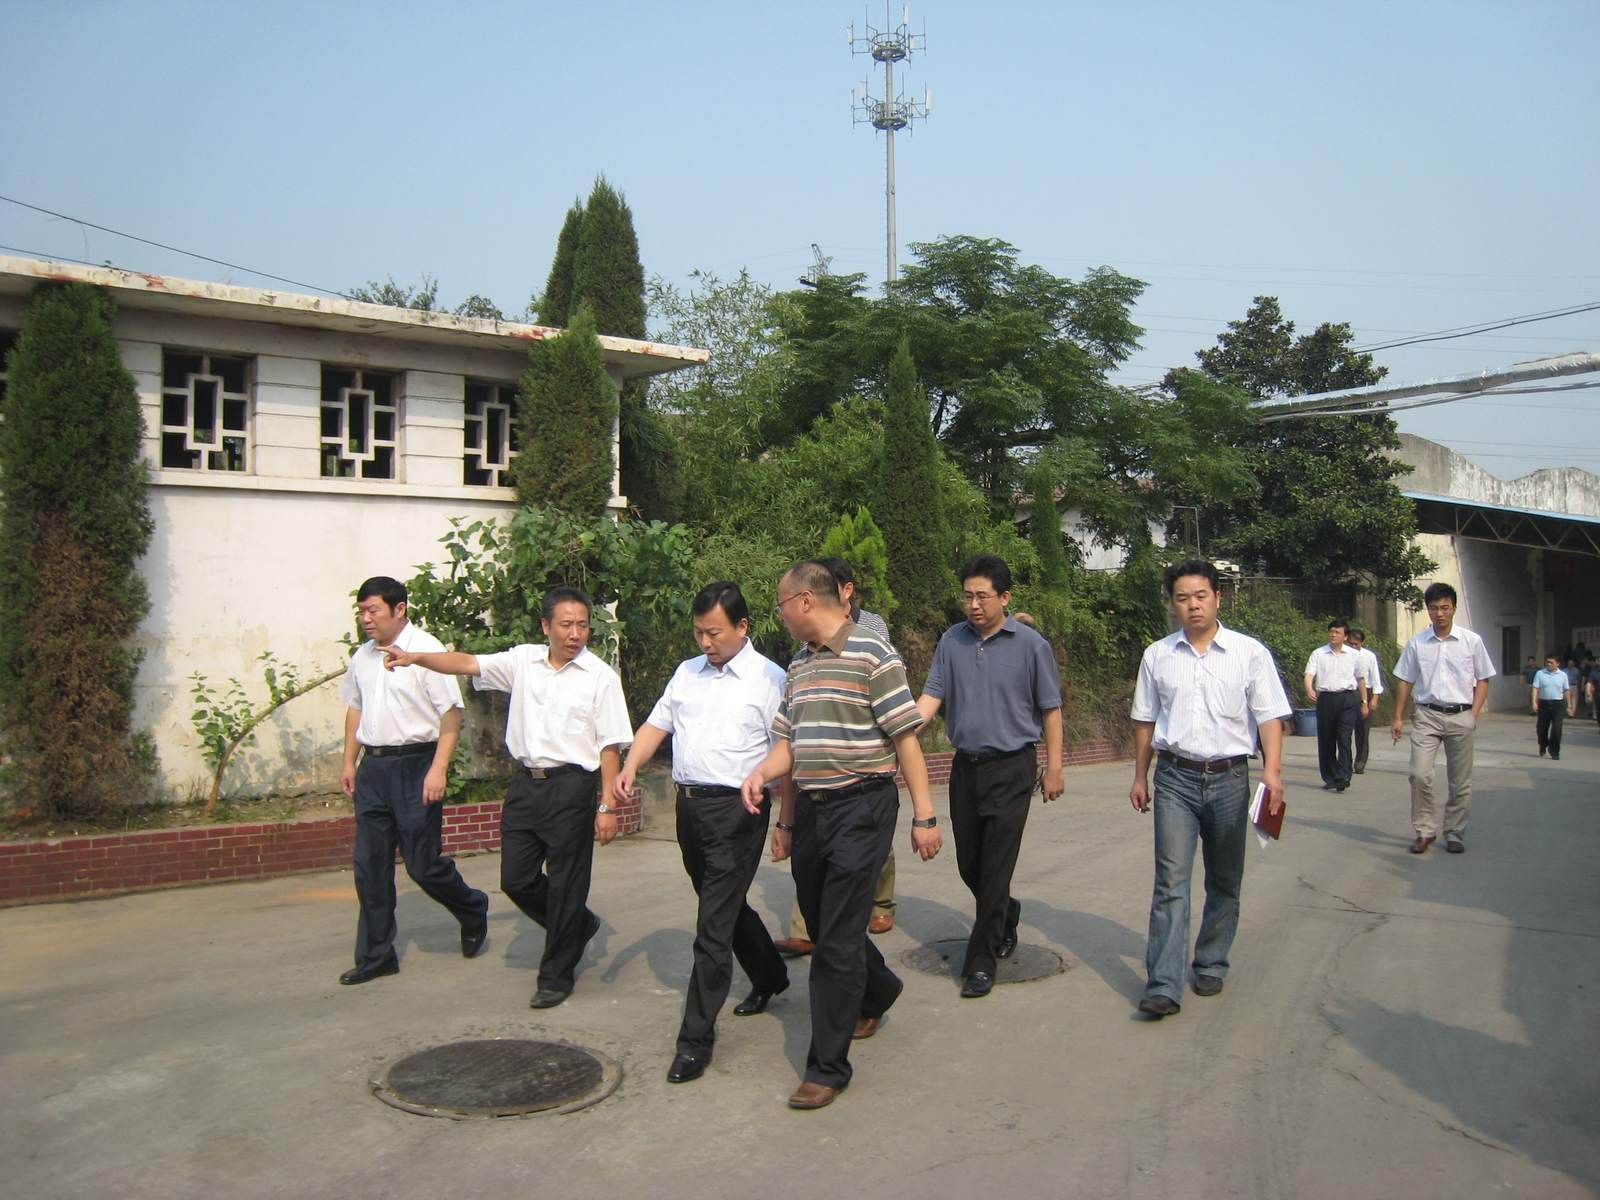
Shows official visits, customer reception, and external communication.

